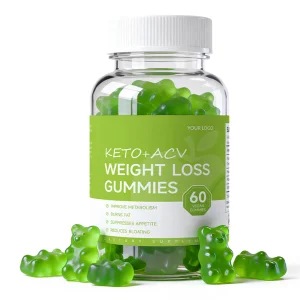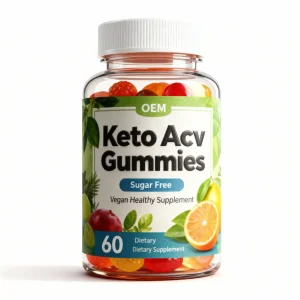
Sugar Free Keto Apple Cider Vinegar Gummies Vegan Acv Weight Management Supplement OEM ODM Factory
View Details
Soybean Enzymatic Hydrolysate Protein Soy Protein Concentrate Animal Feed Additive Poultry Feed Additives Hydrolysate Powder Feed Enhancing Digestive Health
View Details
Custom Printing Linen Workbook Goal Manifestation Inspirational Diary Mental Health Planner Mindfulness Wellness Journal
View Details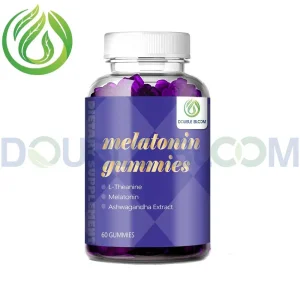
Vegan Melatonin Gummies Supplement Sleep Supplement Melatonin 1omg Dietary Natural Flavor
View DetailsAs international supply chains experience profound structural transformations, global buyers increasingly demand absolute transparency, verifiable scientific efficacy, and strict regulatory adherence. Xian QLU Health Pharmaceutical Technology Co., Ltd. answers this call by bridging traditional botanical wisdom with state-of-the-art chemical engineering.
Grounded in Google Search Quality Rater Guidelines, our digital asset architecture is designed to deliver superior informational depth. We ensure that every B2B procurement specialist discovers verifiable technical parameters, robust safety documentation, and actionable supply chain solutions.
Operating dedicated manufacturing bases strategically located across Shandong, Zhejiang, and Hebei, QLU leverages regional resource advantages to optimize continuous production scaling and mitigate localized operational disruptions.
Our advanced extraction infrastructure integrates automated solvent recovery, supercritical fluid extraction, and high-performance liquid chromatography (HPLC) analytical testing to maintain batch-to-batch consistency.
Strategic positioning near key export hubs coupled with international partnerships in Mumbai and Dubai ensures rapid transit times and agile localized inventory management for global pharmaceutical clients.
The future of herbal extracts relies on marker compound standardization and multi-component fingerprinting. QLU invests heavily in mass spectrometry R&D to isolate minor bioactive constituents that deliver synergistic therapeutic benefits for modern functional foods and pharmaceutical formulations.
Aligning with global net-zero trajectories, our engineering teams are transitioning toward water-based enzymatic extraction techniques and closed-loop solvent systems that drastically reduce carbon footprints while preserving delicate active botanical fractions.
Our production facilities maintain comprehensive compliance credentials including GMP, ISO, FAMI-QS, KOSHER, and HALAL, providing seamless regulatory clearance for importers across North America, Europe, and Asia.
We supply custom formulations, bulk ingredients, and OEM/ODM finished formats tailored to diverse sectors including nutraceuticals, dietary supplements, functional beverages, veterinary care, and cosmetics.
Through strategic marketing hubs in Mumbai and Dubai alongside our Xi'an headquarters, we deliver responsive technical support, documentation dossiers, and flexible supply agreements.
Since our inception, QLU has consistently expanded its operational scope through dedicated investment in research, advanced manufacturing technology, and global network expansion.
Initial foundational focus on pharmaceutical products, food ingredients, and vitamins.
Expanded global marketing operations for APIs, functional ingredients, and chemical intermediates.
Scaled integrated production capabilities across specialized manufacturing facilities.
Consolidated full-spectrum R&D, production, and marketing of advanced APIs and botanical extracts.
In the rapidly evolving pharmaceutical and wellness sector, QLU’s corporate spirit is defined by adaptability, precision engineering, and customer-centric innovation. We actively integrate emerging scientific discoveries to satisfy the exacting standards of modern healthcare providers and global consumers.

We combine multi-base manufacturing infrastructure (Shandong, Zhejiang, Hebei) with rigorous analytical quality control, full international certifications (GMP, ISO, Halal, Kosher), and robust global logistics networks centered out of Xi'an, Mumbai, and Dubai.
Yes. All our production facilities operate under stringent quality management systems certified by international authorities, ensuring seamless export compliance for pharmaceutical, nutraceutical, and food ingredient applications.
We offer comprehensive OEM and ODM solutions, tailoring active ingredient concentrations, delivery formats (powders, tablets, gummies, capsules), and clean-label specifications to match your exact brand requirements.
Through advanced HPLC testing, supercritical extraction methods, and end-to-end supply chain tracking from raw botanical cultivation to final packaging, guaranteeing uniform potency and safety.
 QLU Health